 fuyuhuaxue@iumrs.com

Walk into a commercial office and the floor is speaking before anyone says a word. It’s telling visitors how the company operates—whether it’s organized or chaotic, whether it invests in quality or settles for adequate, whether it’s a place where detail matters or a place where detail is optional. Most businesses never think about this. The ones that do understand something their competitors don’t: the floor is the most-viewed, least-examined surface in the entire building, and it shapes perception in ways that furniture and branding never quite manage.
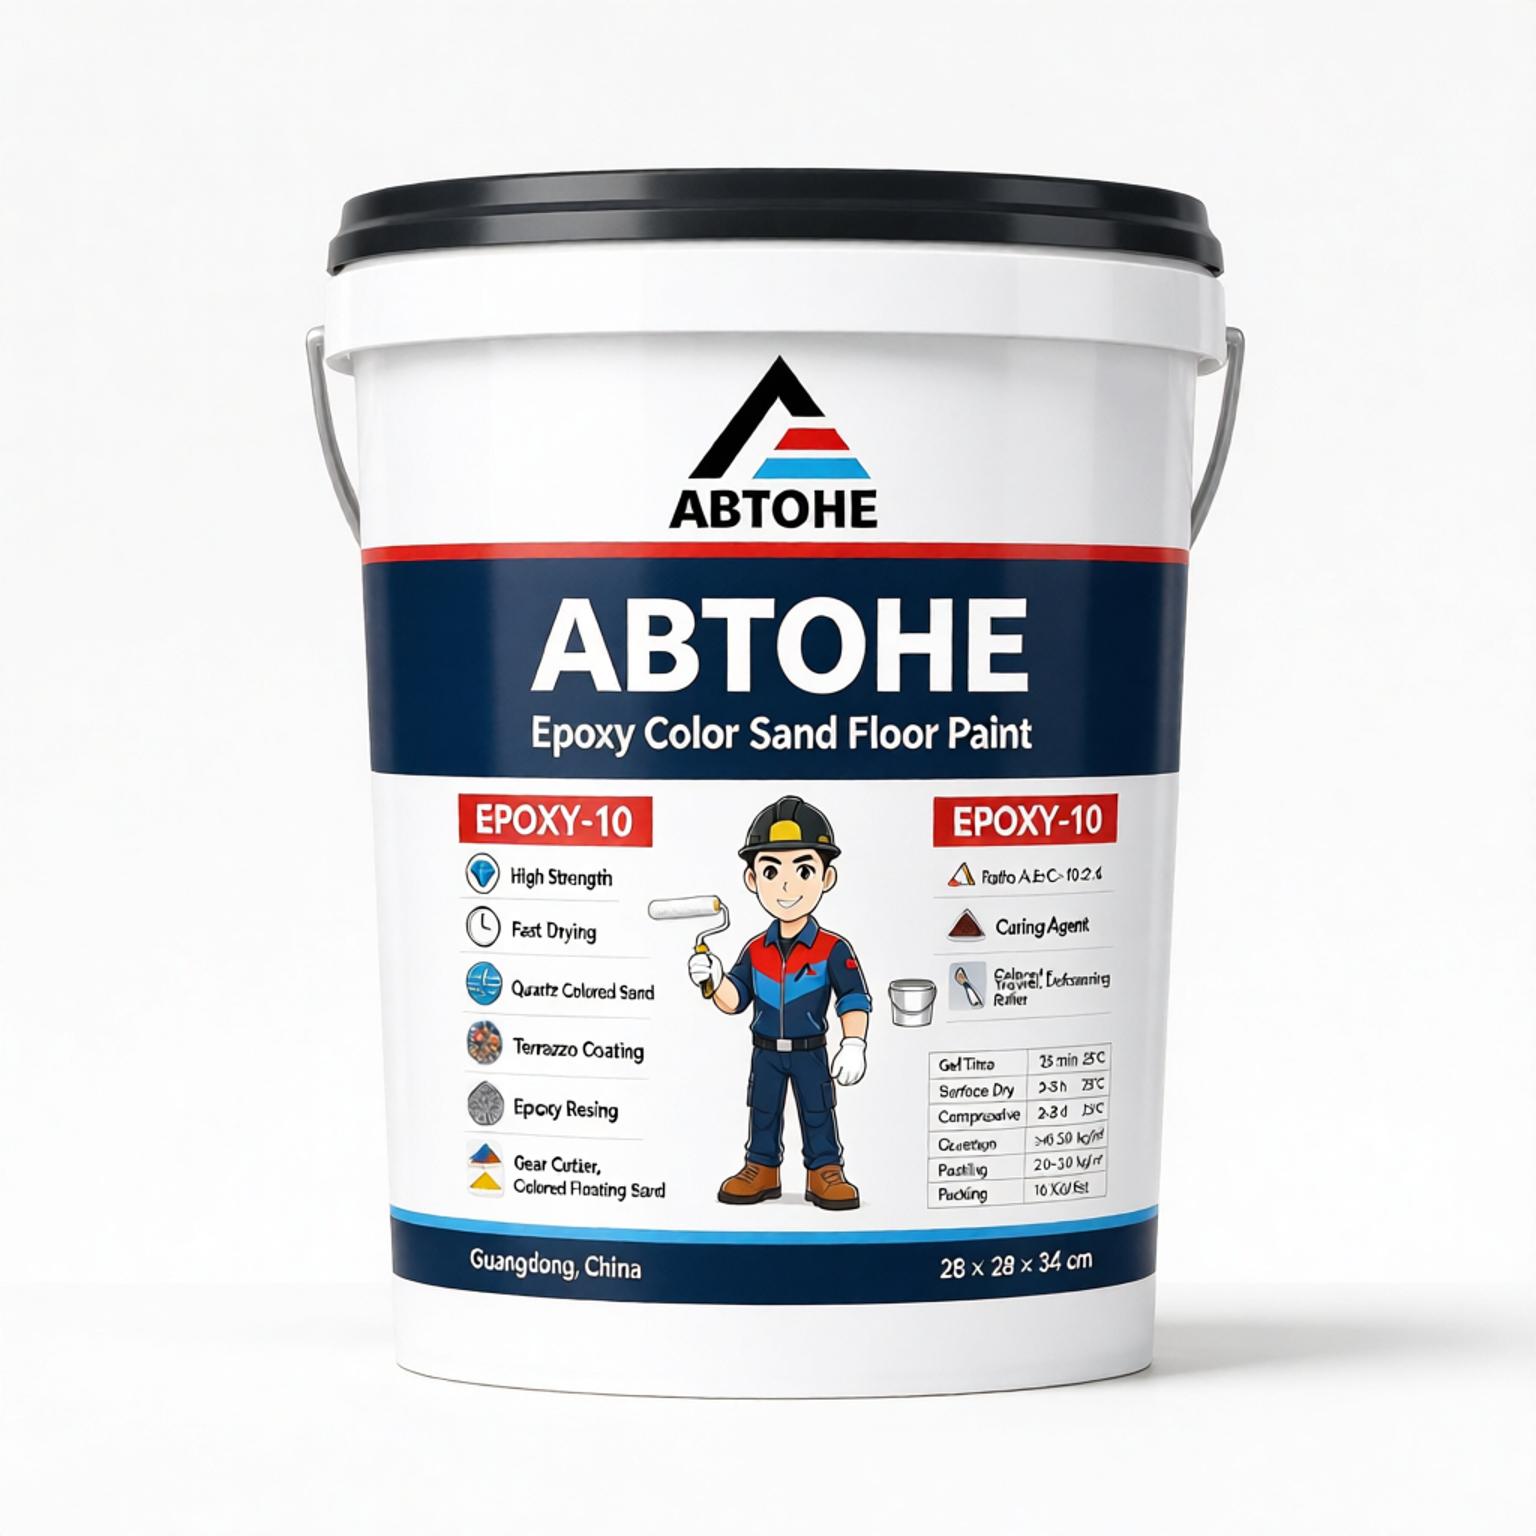
That’s the space the ABTOHE Epoxy Colored Sand Self-Leveling Flooring was designed for. It’s a two-component epoxy system—epoxy resin, curing agent, and colored quartz sand—that cures into a liquid marble-effect, high-gloss, wear-resistant surface with an 80 MPa compressive strength, low VOC content, and customizable RAL/Pantone colors.
Manufactured in Hebei, China, under the ABTOHE brand, supplied as a practical 20kg kit, and backed by OEM support and a 12-month shelf life, it’s a flooring system built for industrial plants, commercial spaces, and residential applications—a product that refuses to choose between the durability of a working floor and the appearance of a design feature.
Let’s explore what makes it worth specifying—and why commercial offices, in particular, should be paying attention.
The Marble Effect: A Floor That Earns Its Compliments
The defining visual characteristic of this product is its liquid marble effect—a finish that resembles natural stone without the weight, cost, or installation complexity of actual marble.
The effect comes from the chemistry. Colored quartz sand is distributed through the epoxy matrix, and as the self-leveling formula flows out and cures, the aggregate settles into a speckled, veined pattern with genuine depth. It’s not a printed image or a surface film. It’s physical material suspended in a cured resin, which means the pattern has weight, movement, and character that a printed product simply cannot match.
For a commercial office, that’s a meaningful upgrade. A high-gloss marble-effect floor reflects light beautifully, brightens the space, and makes the room feel larger and more expensive. It signals investment—the kind of detail clients notice when they walk in for a meeting and the kind of detail employees appreciate in a space where they spend forty hours a week.
And because the color comes from mineral aggregate rather than surface pigment, it holds up over time. The floor doesn’t fade in traffic lanes or lose its pattern where chairs roll. The appearance is part of the floor’s structure, not a decorative layer that can be worn away.
Compressive Strength ≥80 MPa: Built for Real Commercial Use
Visual appeal is easy. Structural performance is harder.
This system delivers a compressive strength of ≥80 MPa (ASTM C579 test)—a specification that places it firmly in industrial territory. In practical terms, that means:
- Furniture and equipment don’t leave permanent indentations
- Rolling loads—carts, chairs, delivery equipment—don’t wear through the surface
- Dropped objects are less likely to cause damage
- Foot traffic in high-volume areas doesn’t degrade the finish
For a commercial office, that durability matters more than people expect. An office isn’t a quiet, low-traffic environment—it’s a place where chairs roll constantly, where deliveries come through, where equipment gets moved, and where the floor is expected to stay presentable through years of use. A coating that can’t bear load will fail quietly, and then loudly, and then expensively.
80 MPa compressive strength is the kind of specification that separates a floor you install once from a floor you replace every few years.
Wear Resistance: Taber Tested to ≤0.02g/1000r
Compressive strength tells you how much load a floor can bear. Abrasion resistance tells you how well it survives the constant friction of daily use.
This product is tested to ≤0.02g/1000r on the Taber abrasion test—a very low abrasion loss, which means the surface resists wear from traffic, grit, and cleaning. The coating stays smooth and glossy rather than developing the dull, patchy appearance of a worn floor.
For a commercial office, that means:
- Traffic lanes stay consistent rather than showing wear paths
- The gloss finish stays reflective rather than turning matte in high-use areas
- Cleaning remains effective because the surface isn’t degrading
- Appearance holds up over years rather than months
Abrasion resistance is the specification that determines whether a beautiful floor still looks beautiful after a few years of use. This product is built to pass that test.
Low VOC: ≤10 g/L
Indoor air quality is no longer a niche concern. Building occupants, tenants, and facility managers increasingly care about what’s in the materials around them—and commercial offices are held to higher standards because they’re spaces where people spend significant time.
This coating delivers a VOC content of ≤10 g/L, compliant with GB/T 38597. That’s genuinely low—well below the thresholds that would classify a product as high-emission, and low enough to make it suitable for indoor use in occupied or soon-to-be-occupied spaces.
For a commercial office, that matters in several ways:
- Less odor during application—important when a floor project is happening in a building that needs to reopen quickly
- Better indoor air quality after curing—important for employees and visitors
- Compliance with green building standards and corporate sustainability targets
- Safer application for the crews doing the work
Low VOC isn’t just a regulatory checkbox. It’s a practical advantage that makes the product easier to specify, easier to install, and easier to live with.
Self-Leveling: Even Results Without Leveling Tools
The product’s self-leveling finish is one of its most practical features. After the two components are mixed and applied, the coating ensures even floors with no need for leveling tools—it flows out and settles into a flat, uniform film on its own.
That self-leveling behavior delivers several benefits for a commercial project:
Speed. The material does the leveling work, so applicators move through the project faster.
Consistency. Uniform thickness means uniform performance—no thin spots that wear early, no thick spots that cure unevenly.
Smoothness. The result is a flat, mirror-like surface that reflects light beautifully and looks professionally installed.
Accessibility. Self-leveling behavior is forgiving, which makes the product accessible to DIY enthusiasts as well as professional contractors.
The application method is a two-component mix applied as a 2K self-leveling system, with a pot life of 30–45 minutes at 25°C—a practical working window for placing a section. Light traffic is possible in 24 hours, with full cure in 7 days at 25°C, which means a commercial floor can be back in service quickly.
Chemical Resistance: Minimal Maintenance
Commercial floors get exposed to everything—cleaning chemicals, coffee spills, ink, oil, and the general debris of daily operations. A coating that can’t resist those substances will stain, soften, or degrade.
This product is resistant to oil, acids, alkalis, and common cleaners, which means spills stay on the surface where they can be wiped up rather than soaking in and causing damage. The floor stays presentable with minimal maintenance—a significant advantage for commercial spaces where cleaning labor is a recurring cost.
That chemical resistance also protects the substrate beneath. A floor that resists chemicals keeps the concrete sealed and protected, which extends the life of the slab and avoids the costly cycle of repair and replacement.
Anti-Slip: R10–R13, Adjustable by Sand Size
Safety is a requirement in any commercial space, and slip resistance is a core part of that.
This product delivers R10–R13 slip resistance, adjustable by sand size—which means the traction can be tuned to the specific demands of the environment. A high-gloss office floor might use a finer sand for a smoother appearance with adequate grip, while a commercial kitchen or wet area might use a coarser aggregate for maximum traction.
That adjustability is valuable for designers and contractors because it allows one product to serve multiple applications without compromising either appearance or safety.
Color Customization: RAL and Pantone
The product is available with RAL and Pantone color customization and OEM support, which means the floor can be matched precisely to a design palette, a brand identity, or a project specification.
For a commercial office, that’s more than decoration. Color shapes how a space feels, how it’s navigated, and how it’s perceived. A floor matched to the brand palette creates cohesion; a floor used for functional zoning supports wayfinding; a floor chosen for warmth or calm affects how employees feel in the space.
Custom color capability turns the floor from a fixed product into a design tool.
Coverage Rate and Packaging
The coverage rate is 0.8–1.2 kg/m² per 1mm thickness, which provides a practical basis for estimating material quantities based on project area and target film thickness. That makes quoting and procurement straightforward for contractors and project buyers.
The product is supplied as a 20kg kit—a practical size for both smaller commercial projects and as a unit of ordering for larger installations. The shelf life is 12 months in the original sealed package, allowing for sensible stock management.
Where This Floor Belongs
The product is designed for industrial plants, commercial spaces, and residential applications, with a feature set that fits:
- Commercial offices – high-gloss marble effect with durability for daily traffic
- Showrooms and retail spaces – reflective finish that elevates displays
- Reception areas and lobbies – a floor that creates a strong first impression
- Industrial plants – 80 MPa compressive strength and chemical resistance
- Residential spaces – decorative and easy to maintain
- High-traffic areas – wear-resistant and minimal maintenance
The Technical Snapshot
- Brand: ABTOHE
- Product: Epoxy Colored Sand Self-Leveling Flooring
- Other Names: Epoxy Colored Sand Self-Leveling Floor Coating
- Place of Origin: Hebei, China
- Main Raw Material: Epoxy Resin + Curing Agent + Colored Quartz Sand
- State: Liquid (Two-Component) / Ready-to-Mix Slurry
- Application Method: 2K Self-Leveling Application / Two-Component Mix
- CAS No.: 61788-97-4
- EINECS No.: 500-148-2
- Molecular Formula: C18H20O3
- Compressive Strength: ≥80 MPa (ASTM C579)
- Wear Resistance: ≤0.02 g/1000r (Taber Abrasion Test)
- VOC Content: ≤10 g/L (Low VOC, GB/T 38597 compliant)
- Pot Life: 30–45 mins at 25°C
- Full Cure Time: 7 days at 25°C (Light Traffic in 24h)
- Coverage Rate: 0.8–1.2 kg/m² per 1mm Thickness
- Color Customization: RAL / Pantone Colors Available, OEM Supported
- Anti-Slip Performance: R10–R13 Slip Resistance (Adjustable by Sand Size)
- Chemical Resistance: Resistant to oil, acids, alkalis, and common cleaners
- Shelf Life: 12 Months in Original Sealed Package
- Usage: Industrial Plants, Commercial Spaces, Residential
- Packaging: 20kg kit, single item
Key advantages:
- Self-leveling finish for even floors without leveling tools
- Durable epoxy coating for long-lasting protection against wear and tear
- Easy application with a smooth process for DIY enthusiasts
- Color options in various vibrant epoxy colors for aesthetic appeal
- Chemical resistance for high-traffic areas with minimal maintenance
- Liquid marble effect for a high-end decorative appearance
Who This Floor Is For
Commercial office managers and facility directors who want a floor that reflects the quality of the business and holds up to daily use.
Interior designers and architects specifying a high-gloss marble-effect finish with customizable RAL/Pantone colors.
Contractors who need a self-leveling, fast-curing system with clear technical specifications and reliable performance.
Distributors and importers seeking a factory-direct product with OEM support, low VOC compliance, and broad application across commercial, industrial, and residential markets.
DIY users who want a professional-grade floor that’s genuinely achievable with a smooth, forgiving application process.
The Bottom Line
A commercial floor is a long-term commitment. It’s the surface every client walks on, every employee works on, and every piece of furniture and equipment rolls across. It shapes how a space feels, how it functions, and how much it costs to maintain.
The ABTOHE Epoxy Colored Sand Self-Leveling Flooring is built for that long-term view. It delivers a liquid marble effect with high-gloss reflective beauty, ≥80 MPa compressive strength for heavy loads, Taber-tested wear resistance for daily traffic, low VOC content (≤10 g/L) for indoor air quality, self-leveling application for even, professional results, chemical resistance for minimal maintenance, R10–R13 adjustable slip resistance for safety, and RAL/Pantone color customization with OEM support.
It’s manufactured in Hebei, China, supplied as a practical 20kg kit, and backed by a 12-month shelf life.
If you’re choosing a floor for a commercial office, a showroom, or any space where appearance and performance both matter, this is the product that makes the decision easy—and the results unforgettable.
ABTOHE Epoxy Colored Sand Self-Leveling Flooring. Marble beauty. Epoxy strength. A floor that works as hard as the business above it.