 fuyuhuaxue@iumrs.com

Warehouse floors live a life of quiet punishment. They absorb the weight of loaded pallets, the constant roll of forklift wheels, the drip of oils and chemicals, the scuff of boots, and the relentless cycle of cleaning. They do all of this without complaint, without maintenance schedules, and without anyone really noticing them—until something goes wrong.
And when a warehouse floor goes wrong, it goes wrong loudly. A crack becomes a trip hazard. A peeling edge becomes a contamination source. A dusting slab becomes a quality-control problem. A slippery patch becomes an insurance claim. Suddenly, the floor that nobody thought about is the only thing anyone is talking about.
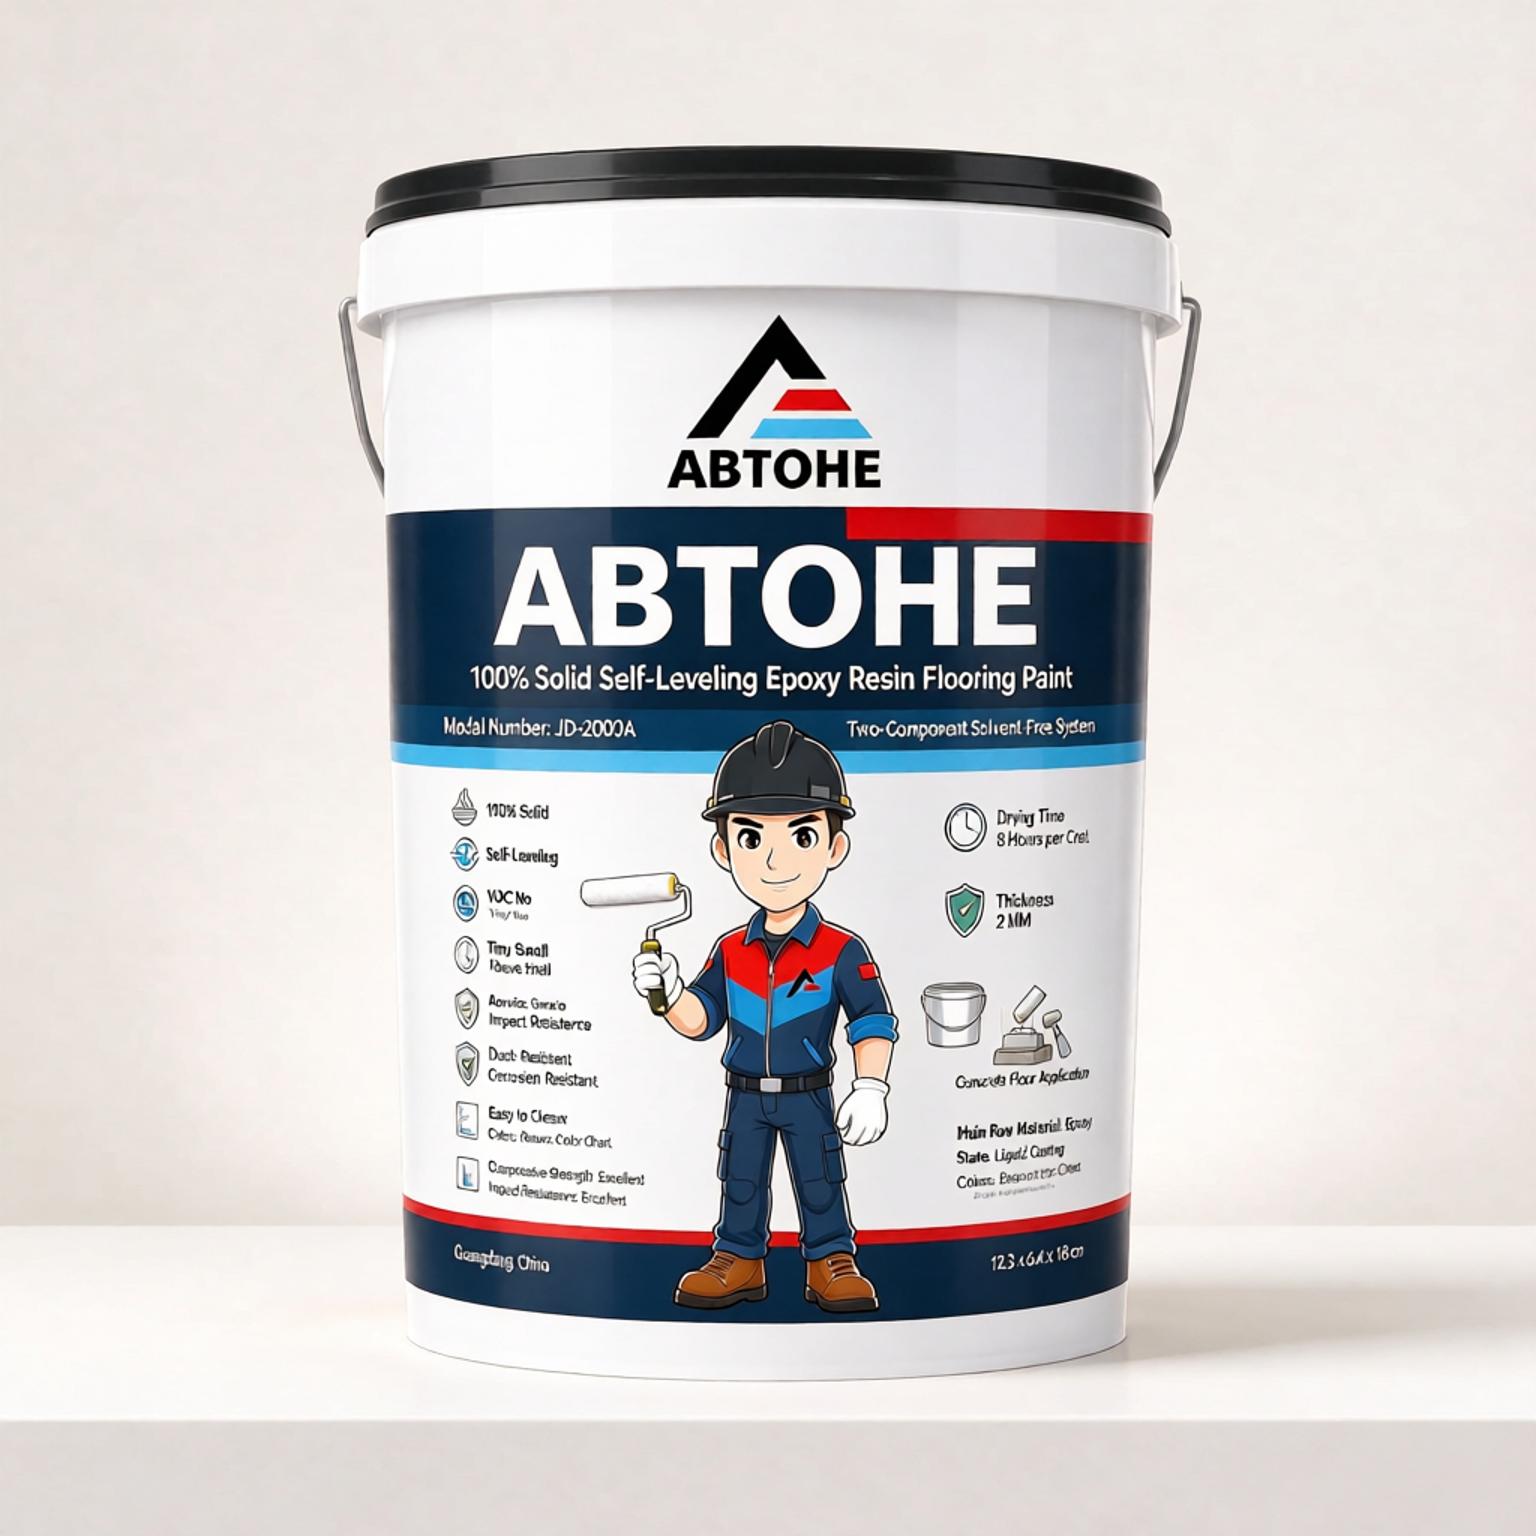
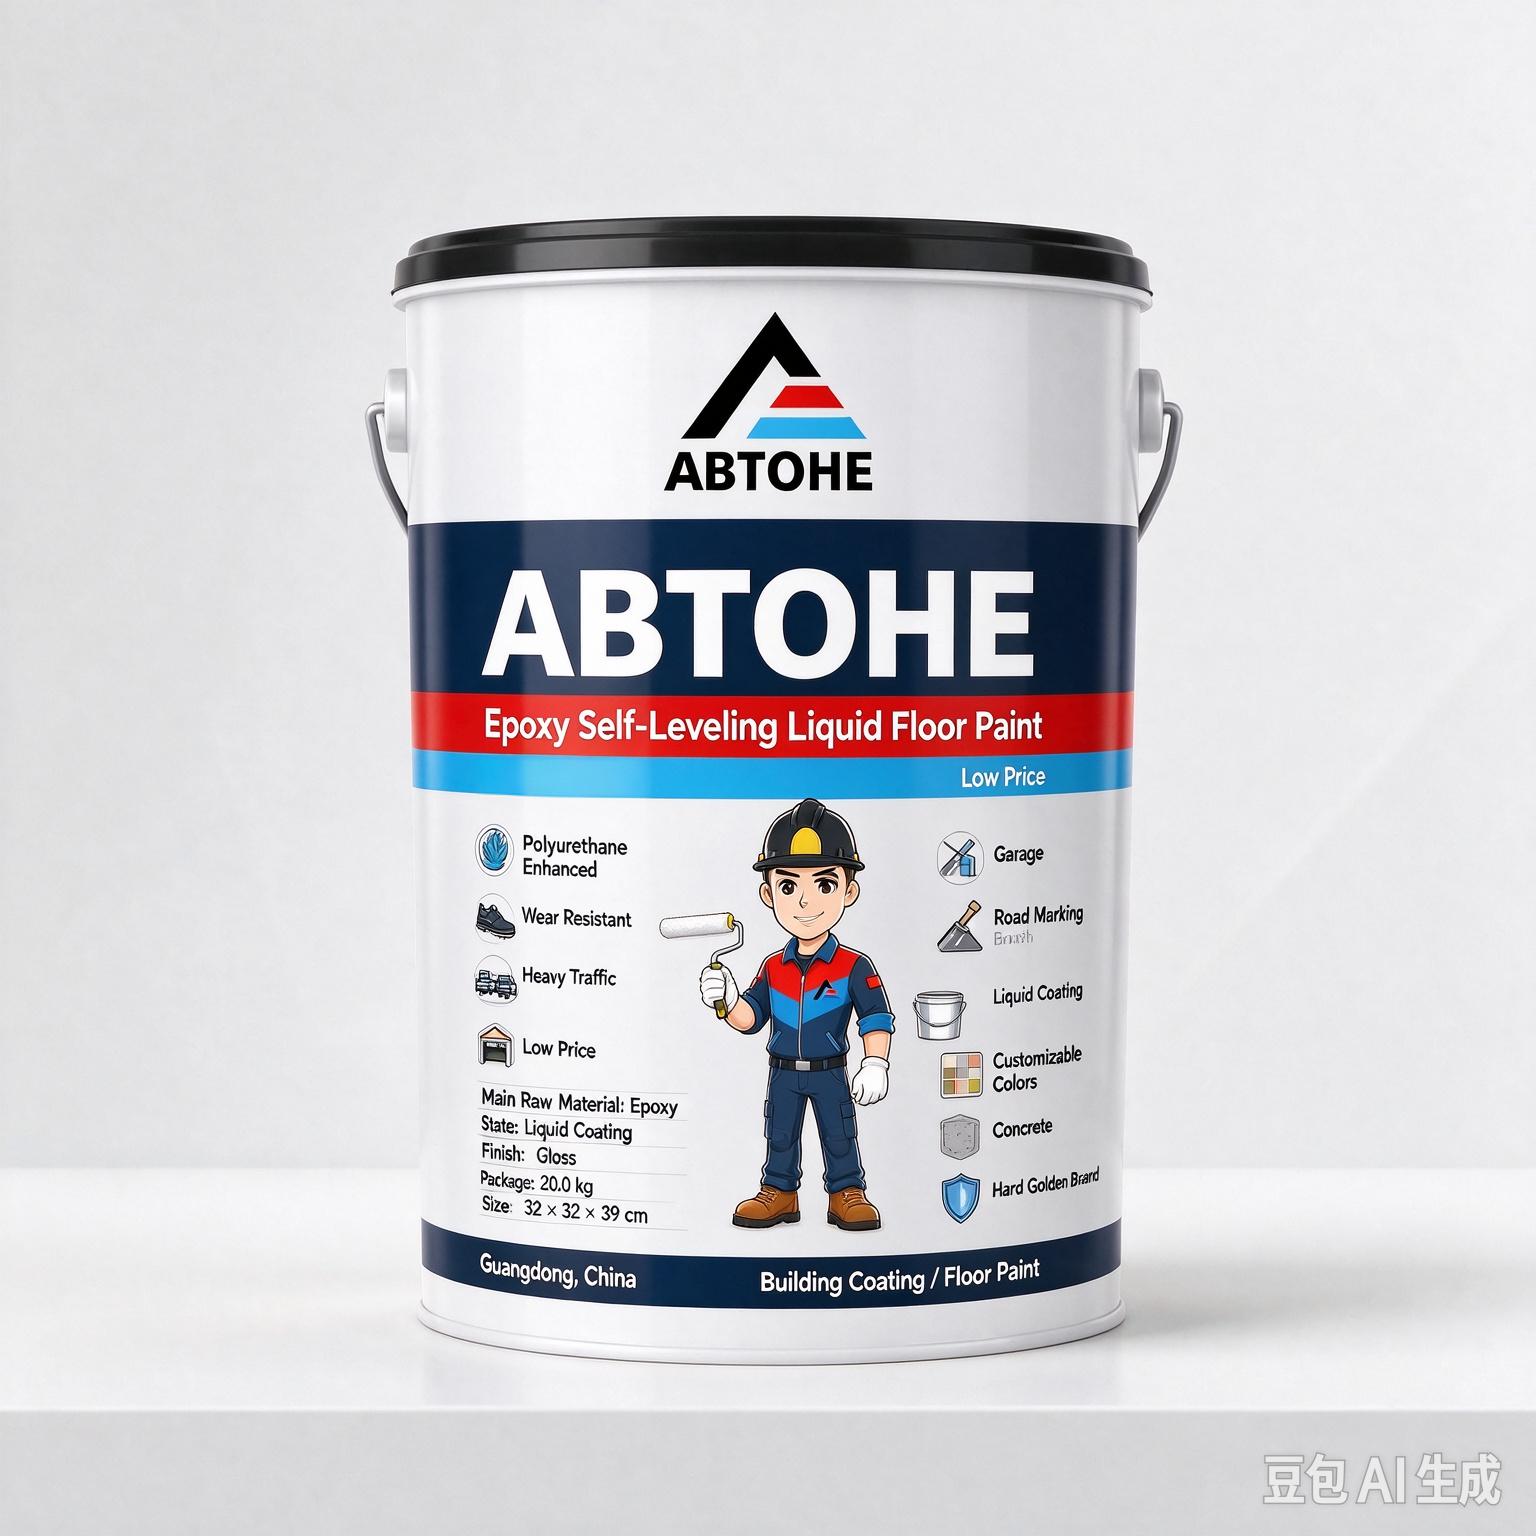
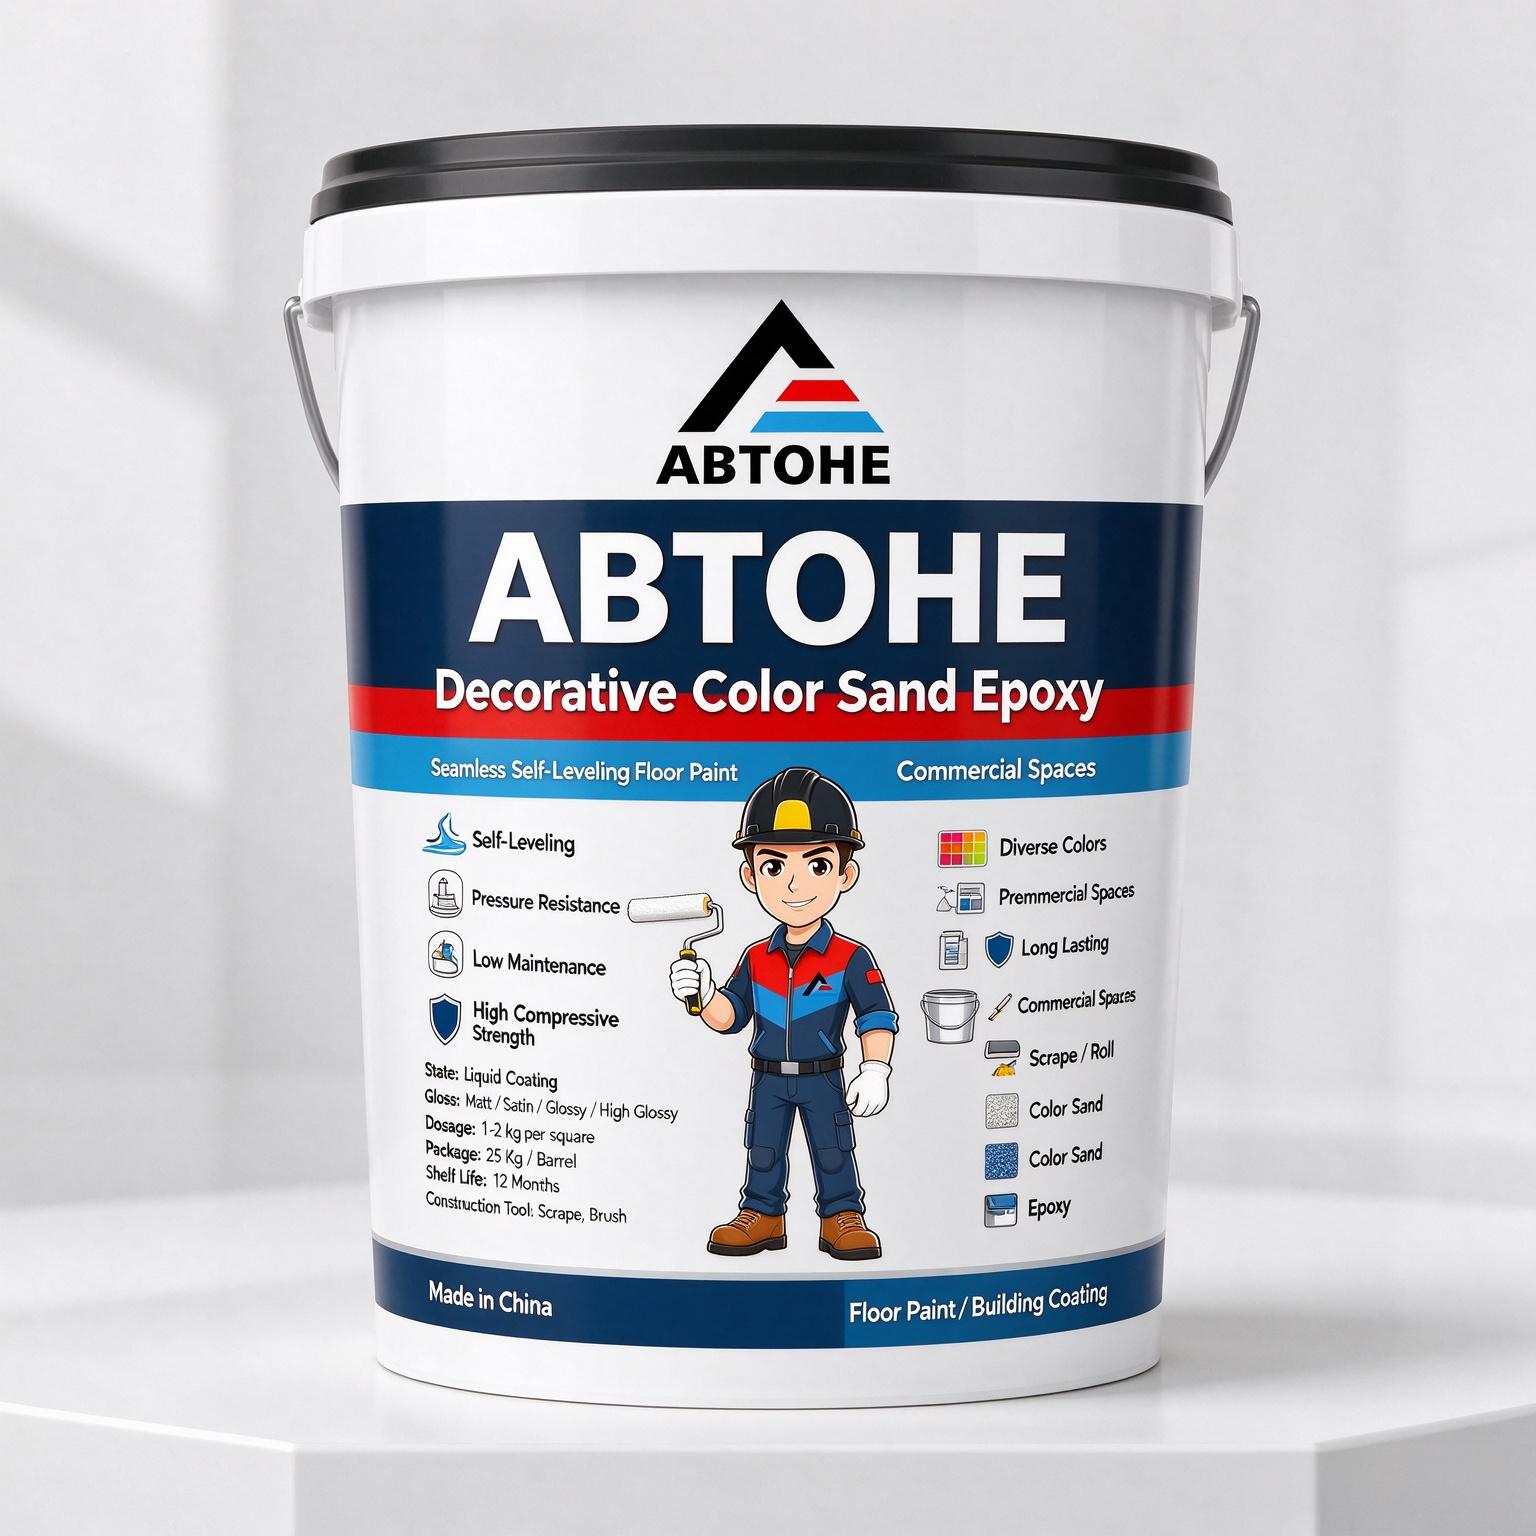
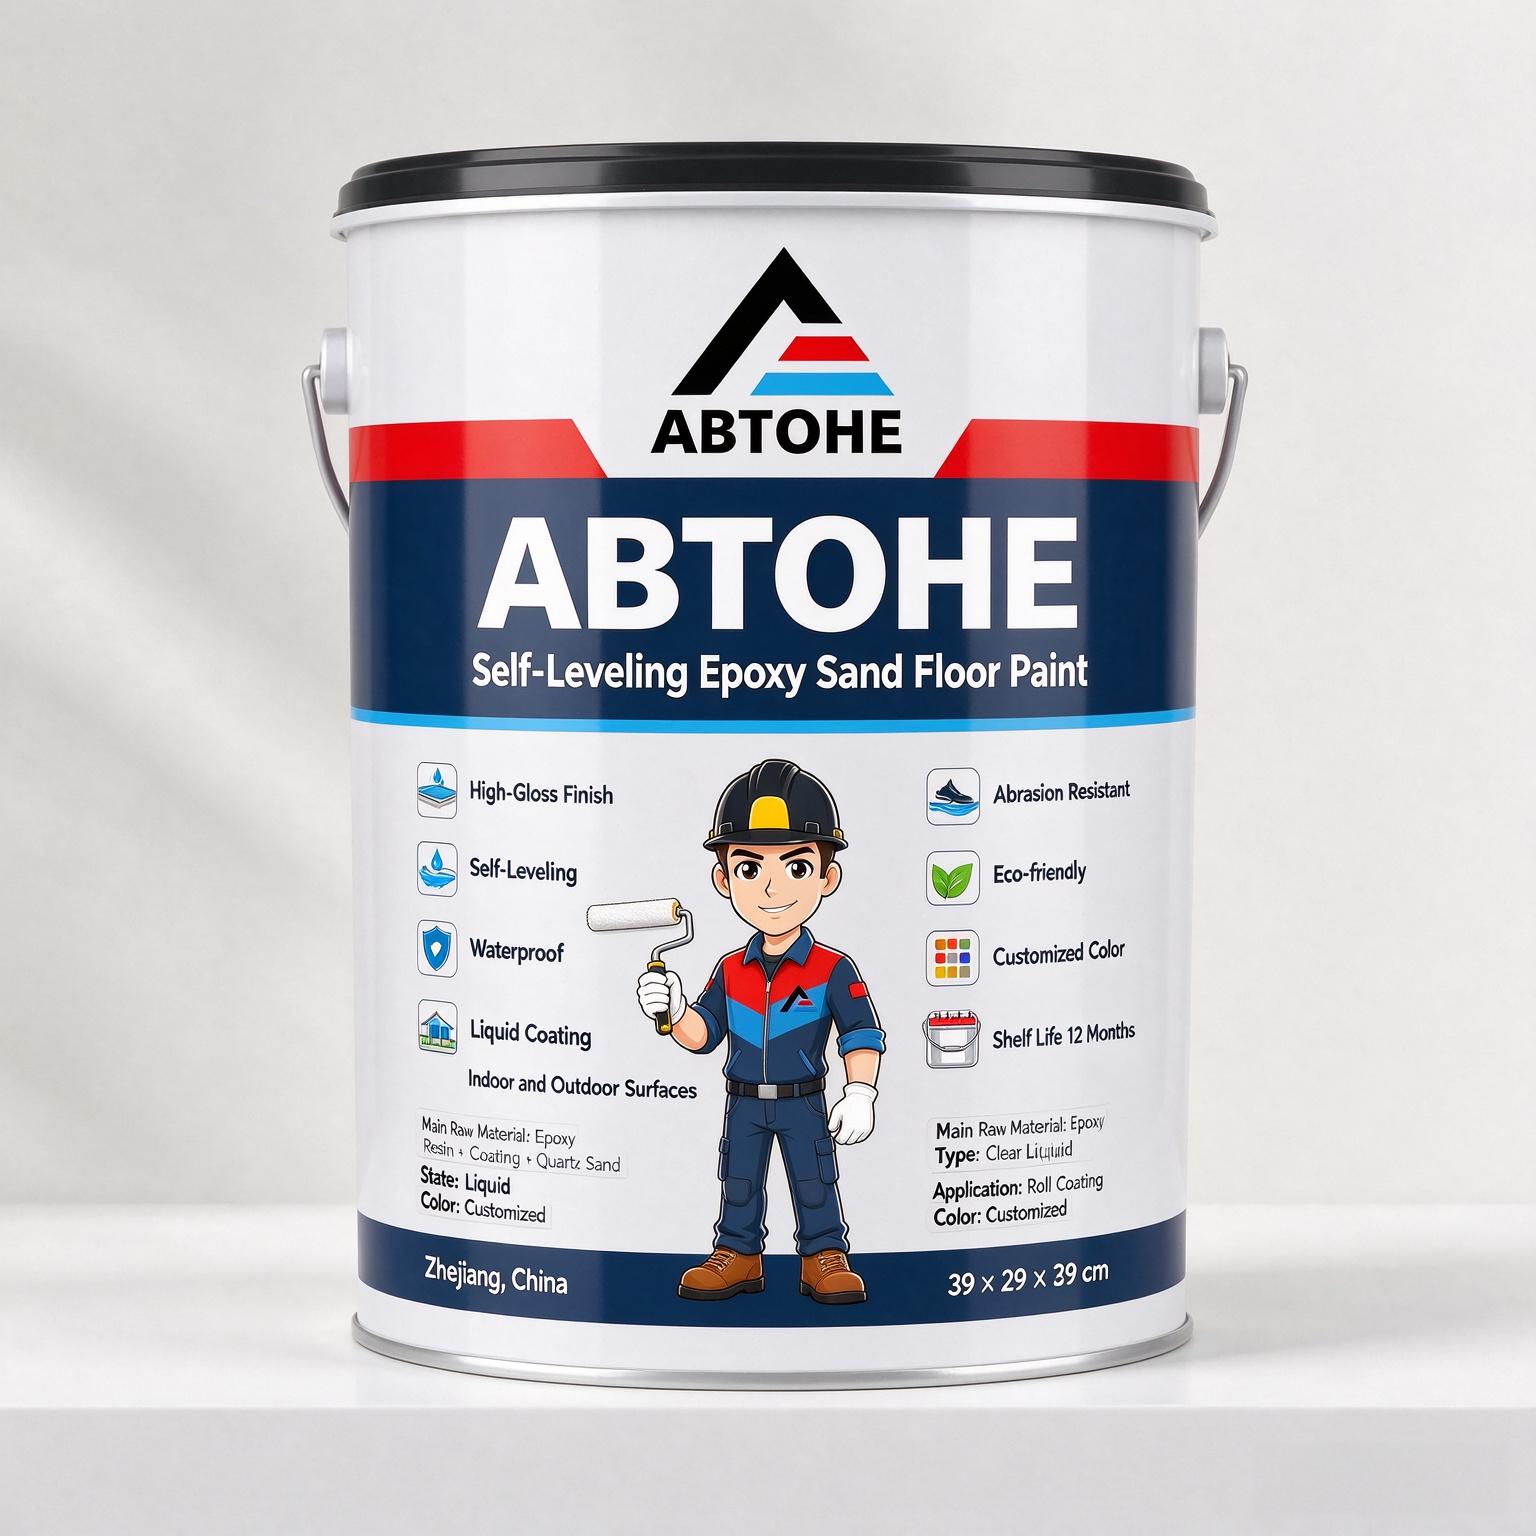
The ABTOHE Waterproof Color Sand Self-Leveling Epoxy Liquid Marble Flooring was engineered for exactly this reality. It’s a heavy-duty epoxy coating designed for warehouses, basements, laboratories, workshops, living rooms, and roofs—a product that combines waterproof protection, self-leveling application, liquid marble aesthetics, and customizable colors into a single system.
Manufactured in Guangdong, China, under the ABTOHE brand, with OEM/ODM support, samples available, and a 20 KG package size, it’s a floor coating built for the punishing realities of industrial and commercial use—while looking good enough for spaces where appearance matters.
Let’s explore why this product deserves a place in your next warehouse project.
High-Performance Epoxy Coating: Durable and Waterproof
The foundation of this product is its high-performance epoxy coating, which provides durable and waterproof protection for floors.
Epoxy resin is the benchmark chemistry for hard, durable, seamless flooring. It bonds strongly to concrete, cures into a dense film, and resists the wear, impact, and chemical exposure that destroy lesser coatings. It’s the material that industrial floors have relied on for decades—and for good reason.
The waterproof quality is equally important. Warehouses are exposed to moisture from multiple sources: humidity, wash-downs, spills, roof leaks, and groundwater. A floor that doesn’t resist moisture allows water to penetrate the concrete, causing efflorescence, weakening the slab, and destroying the coating from below.
This product seals the surface against moisture, protecting the concrete beneath and keeping the floor functional and cleanable. Spills sit on top where they can be wiped up rather than soaking in. The floor stays dry, stable, and presentable.
The formulation combines epoxy resin with a waterborne hardener, which offers a balance of performance and practicality—strong adhesion, good curing, and a lower-odor profile than solvent-based alternatives.
Self-Leveling Texture: Even Floors Without Extra Work
The self-leveling behavior of this coating is one of its most practical features. After application, the material flows out and settles into a flat, even surface finish without additional leveling steps.
That’s a significant advantage in a warehouse context, where large areas need to be coated efficiently and consistently. Manual leveling is slow, labor-intensive, and prone to error—high spots and low spots that become wear points and puddles. A self-leveling formula eliminates that problem. The coating finds its own level, creating a uniform surface that performs consistently across the entire floor.
The result is a seamless, smooth surface that’s easier to clean, easier to maintain, and more professional in appearance. In a warehouse, that seamless quality also eliminates joints and grout lines where dirt and moisture collect—a meaningful improvement in hygiene and cleanability.
The application method is brush, which is practical for edges, corners, and smaller areas, with roller or squeegee options for larger floors. The self-leveling behavior ensures a smooth result regardless of the application method.
Liquid Marble Aesthetics: A Warehouse Floor That Looks Intentional
Here’s where this product genuinely surprises. It’s not just a functional warehouse coating—it’s a liquid marble flooring with decorative appeal.
The color sand is distributed through the epoxy film, creating a speckled, stone-like appearance with depth and movement. Combined with the self-leveling smoothness, the result reads as liquid marble—a surface with the visual character of natural stone rather than flat, painted concrete.
That decorative quality matters more in a warehouse than you might expect. A well-finished floor signals a well-run operation. It reflects light, brightens the space, and makes the facility look organized and cared for—something that matters during client audits, inspections, and site visits.
And it’s not just about appearance. A high-gloss, seamless surface is easier to clean because dirt and spills sit on top rather than soaking into pores or joints. The floor maintains its appearance with routine maintenance rather than requiring aggressive scrubbing.
Multiple Applications: One Product, Many Spaces
The product is designed for a broad range of applications, making it a versatile choice for distributors, contractors, and facility managers who need one coating that can serve multiple needs.
Basements benefit from the waterproof formulation and seamless surface—ideal for spaces where moisture is a constant concern.
Laboratories require chemical resistance and easy cleanability, both of which this epoxy system delivers.
Workshops need wear resistance and impact resistance to handle tools, equipment, and daily work.
Living rooms and residential spaces benefit from the decorative marble effect and low-maintenance surface.
Roofs benefit from the waterproofing and weather resistance—a practical solution for flat roof protection.
That breadth of application means one product can serve multiple markets, which is efficient for distributors and convenient for contractors.
Customizable Colors: Match Any Design or Brand
The product is available in customized colors, which means the floor can be matched to a design palette, a brand identity, or a functional color-coding scheme.
In a warehouse, color is a tool. Color-coded zones designate walkways, storage areas, hazardous zones, and equipment footprints. Color can improve visibility, reinforce safety protocols, and support wayfinding in large facilities.
In residential and commercial spaces, color is a design decision—shaping how the room feels and how it’s perceived.
Because the color comes from mineral aggregate integrated into the coating rather than a surface pigment, it holds up over time rather than fading in traffic lanes. The floor keeps its character through years of use.
Waterproof Performance: Protection That Matters
The waterproof quality of this coating deserves its own section, because it’s one of the most important performance characteristics for warehouse and industrial applications.
Water is the enemy of concrete floors. It penetrates the surface, causes efflorescence, weakens the slab, and destroys coatings from below. In warehouses, moisture comes from multiple sources: humidity, wash-downs, spills, roof leaks, and groundwater. A floor that doesn’t resist moisture is a floor that’s slowly failing.
This product seals the surface against moisture, protecting the concrete beneath and keeping the floor functional and cleanable. The waterproof barrier also makes the floor easier to clean—spills sit on top where they can be wiped up rather than soaking in.
For basements, roofs, and any space where moisture is a concern, that waterproofing is essential. For warehouses and workshops, it’s the difference between a floor that lasts and one that degrades.
Packaging and Supply
The product is supplied in a 20 KG package, with a single package size of 31 × 31 × 38 cm and a gross weight of 20.0 kg. The MOQ is 28 Kg, with a large MOQ option of 100 kg for bulk orders—making it economical for larger projects.
Storage is in a cool, dry place, and the product is available as a sample for evaluation before commitment. OEM/ODM services are supported, allowing for customized branding and packaging.
That combination of practical packaging, bulk availability, and OEM flexibility makes the product suitable for distributors building a product line, contractors managing projects, and facility managers sourcing for ongoing needs.
Where This Floor Belongs
The application range reflects the product’s versatility:
- Warehouses and distribution centers – heavy-duty wear resistance and waterproof protection
- Basements – moisture-resistant and easy to clean
- Laboratories – chemical-resistant and hygienic
- Workshops – durable under tools, equipment, and daily work
- Living rooms – decorative marble effect with low maintenance
- Roofs – waterproofing and weather resistance
- Industrial facilities – high-performance epoxy for demanding environments
The Technical Snapshot
- Brand: ABTOHE
- Product: Waterproof Color Sand Self-Leveling Epoxy Floor Paint
- Other Names: Liquid Marble Flooring, Warehouse Heavy-Duty Coating
- Place of Origin: Guangdong, China
- Main Raw Material: Epoxy
- Material: Epoxy Resin + Waterborne Hardener
- State: Liquid coating
- Application Method: Brush
- Usage: Building coating, other
- Application: Basement, laboratory, workshop, living room, roof
- Color: Customized
- MOQ: 28 Kg (large MOQ 100 kg for bulk orders)
- Packing: Carton box
- Weight: 20 KG
- Storage: Cool dry place
- Sample: Available
- Service: OEM/ODM
- Packaging: Single item, 31 × 31 × 38 cm, 20.0 kg gross weight
Key advantages:
- High-performance epoxy coating for durable, waterproof floor protection
- Self-leveling texture for even surface finish without additional leveling steps
- Multiple applications for basements, workshops, laboratories, living rooms, and roofs
- Customizable colors to match any decor or functional requirement
- Liquid marble effect for a high-end decorative appearance
- Waterproof and heavy-duty for warehouse and industrial use
- OEM/ODM support with samples available
Who This Floor Is For
Warehouse and facility managers who need a durable, waterproof, easy-clean floor that withstands heavy traffic and chemical exposure.
Contractors who want a self-leveling, brush-applied system that delivers consistent, professional results.
Distributors and importers seeking a factory-direct product with OEM/ODM support, customizable colors, and broad application across industrial, commercial, and residential markets.
Homeowners looking for a decorative, waterproof floor for basements, living rooms, or roofs.
The Bottom Line
A warehouse floor is the platform everything else runs on. When it performs, nobody notices. When it fails, everything suffers—safety, productivity, cleanliness, and the bottom line.
The ABTOHE Waterproof Color Sand Self-Leveling Epoxy Liquid Marble Flooring is designed for the first scenario. It delivers high-performance epoxy protection that’s durable and waterproof, a self-leveling texture for even, seamless results, multiple applications across basements, workshops, laboratories, living rooms, and roofs, customizable colors for any design or functional need, and a liquid marble effect that makes the floor as attractive as it is durable.
It’s manufactured in Guangdong, China, available with OEM/ODM support and samples, and supplied in practical 20 KG packaging with bulk MOQ options.
If your warehouse floor is still bare concrete—dusting, staining, and waiting for its first failure—this is the upgrade that pays for itself quietly, every shift, for years.
ABTOHE Waterproof Color Sand Self-Leveling Epoxy Flooring. Heavy-duty protection. Marble beauty. Built for the floor under the work.